Industrial system sales
Sales and commercial coordination for pyrolysis, biochar and related agricultural or industrial technology.
Mobile, containerized PyroChar 150 technology with ultra-low Total PAH, fully electric ignition and intuitive PLC control — engineered for efficient biomass conversion and practical energy recovery.
Innovative technology · Mobile containerized design · Digital control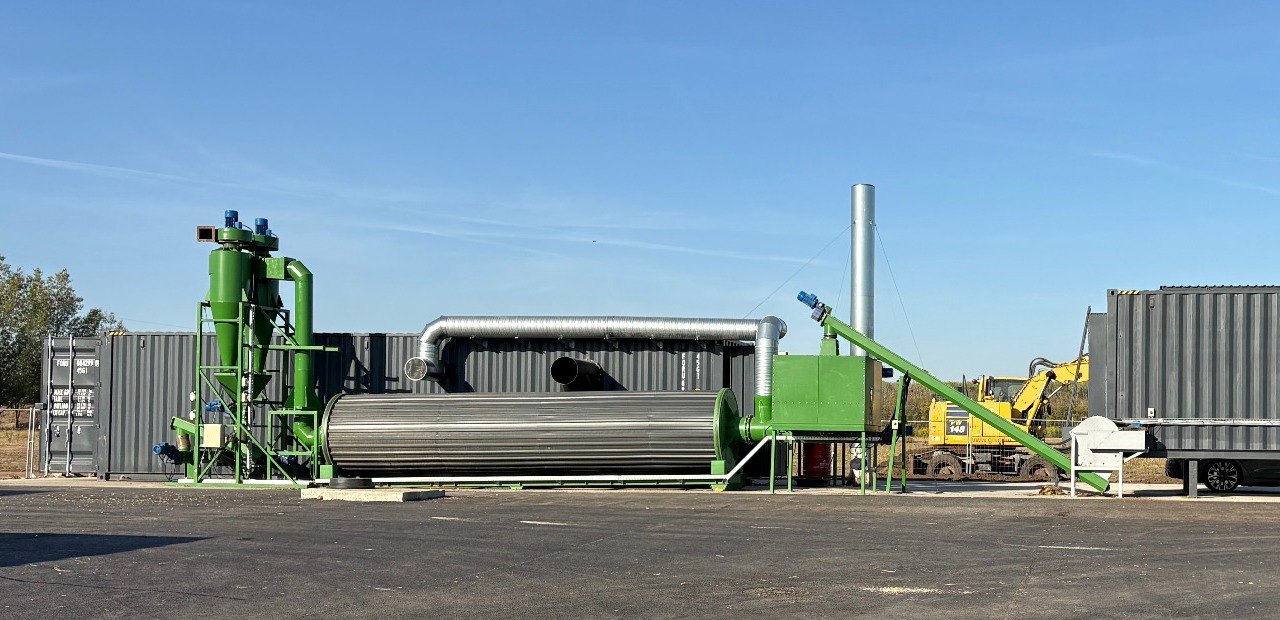
From system sales and commissioning to technical consulting, we connect innovative pyrolysis technology with commercially viable industrial projects.
Sales and commercial coordination for pyrolysis, biochar and related agricultural or industrial technology.
Wholesale and trade intermediation for industrial machinery, process equipment and supporting technical solutions.
Support for commissioning, service, maintenance and equipment-rental arrangements.
Engineering support and consulting on lowering CO₂ footprint through more efficient material flows and energy use.
Clean output, intelligent automation and modular engineering bring practical advantages to modern biochar projects.
Industrial biochar samples measured 0.03–0.08 mg/kg Total PAH — at least 75 times below the 6 mg/kg EBC reference limit shown in the supplied comparison. All tested samples were reported to meet the referenced requirement.
The modular, container-based construction supports transportability, rapid site deployment and simpler relocation when project needs change.
Fully electric ignition eliminates fossil-fuel start-up and contributes to a smaller overall CO₂ footprint for the operating concept.
All sensor readings and operating parameters are visualized in real time through a graphical tablet interface. System functions can be remotely monitored and controlled.
The automation concept can be linked to external monitoring, data-acquisition and validation platforms for transparent process documentation.
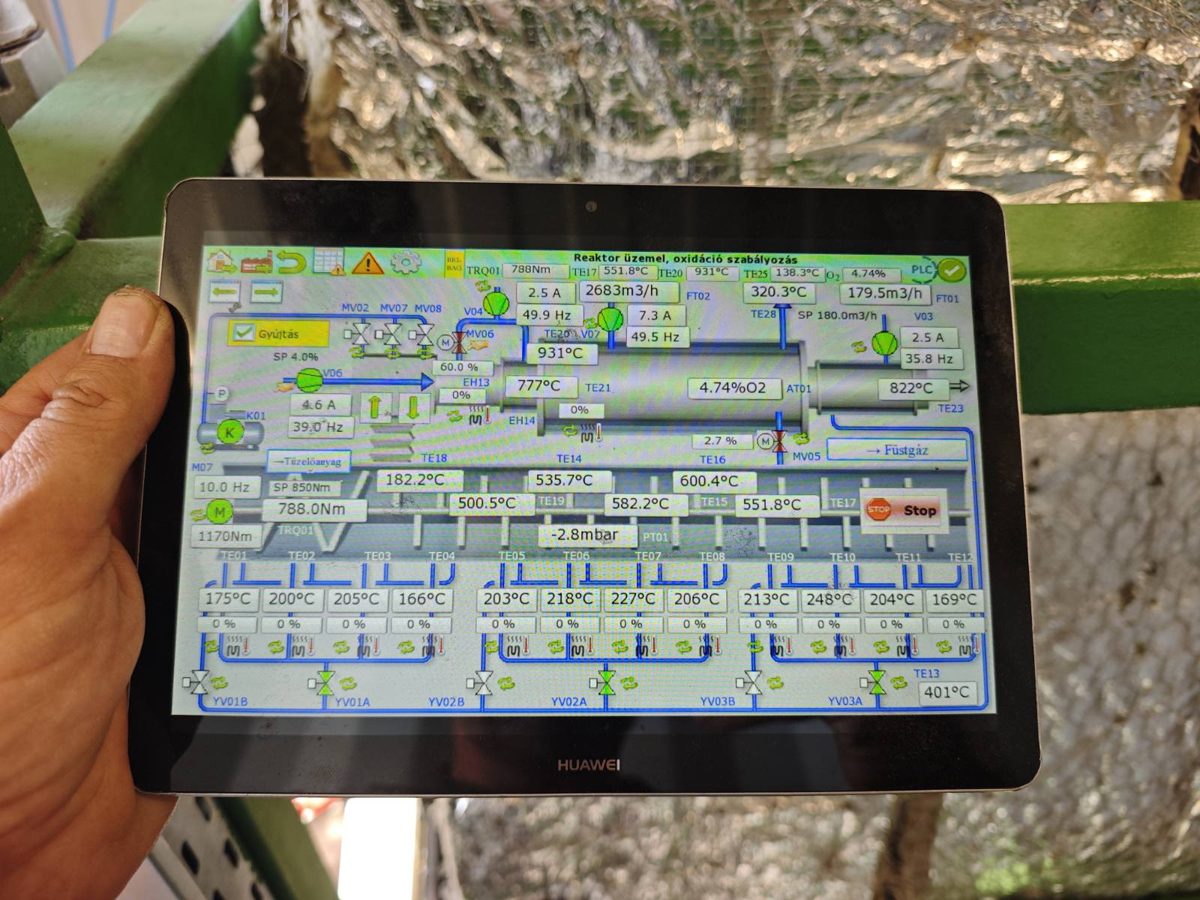
All sensor data and operating parameters remain visible in real time — including remote supervision and control.
The system offers comprehensive PLC control, remote monitoring and remote intervention. All measurement data from the system’s sensors and all key operating parameters are displayed on a graphical tablet interface in real time. Plant functions can also be supervised and controlled remotely.
Industrial biochar samples measured 0.03–0.08 mg/kg Total PAH — at least 75 times below the 6 mg/kg EBC reference limit shown in the supplied comparison. All tested samples were reported to meet the referenced requirement.
At least 75× below the stated reference limit
Comparison refers to the 6 mg/kg Total PAH benchmark in the supplied technical material; applicability depends on the relevant EBC category, analytical method and current criteria.
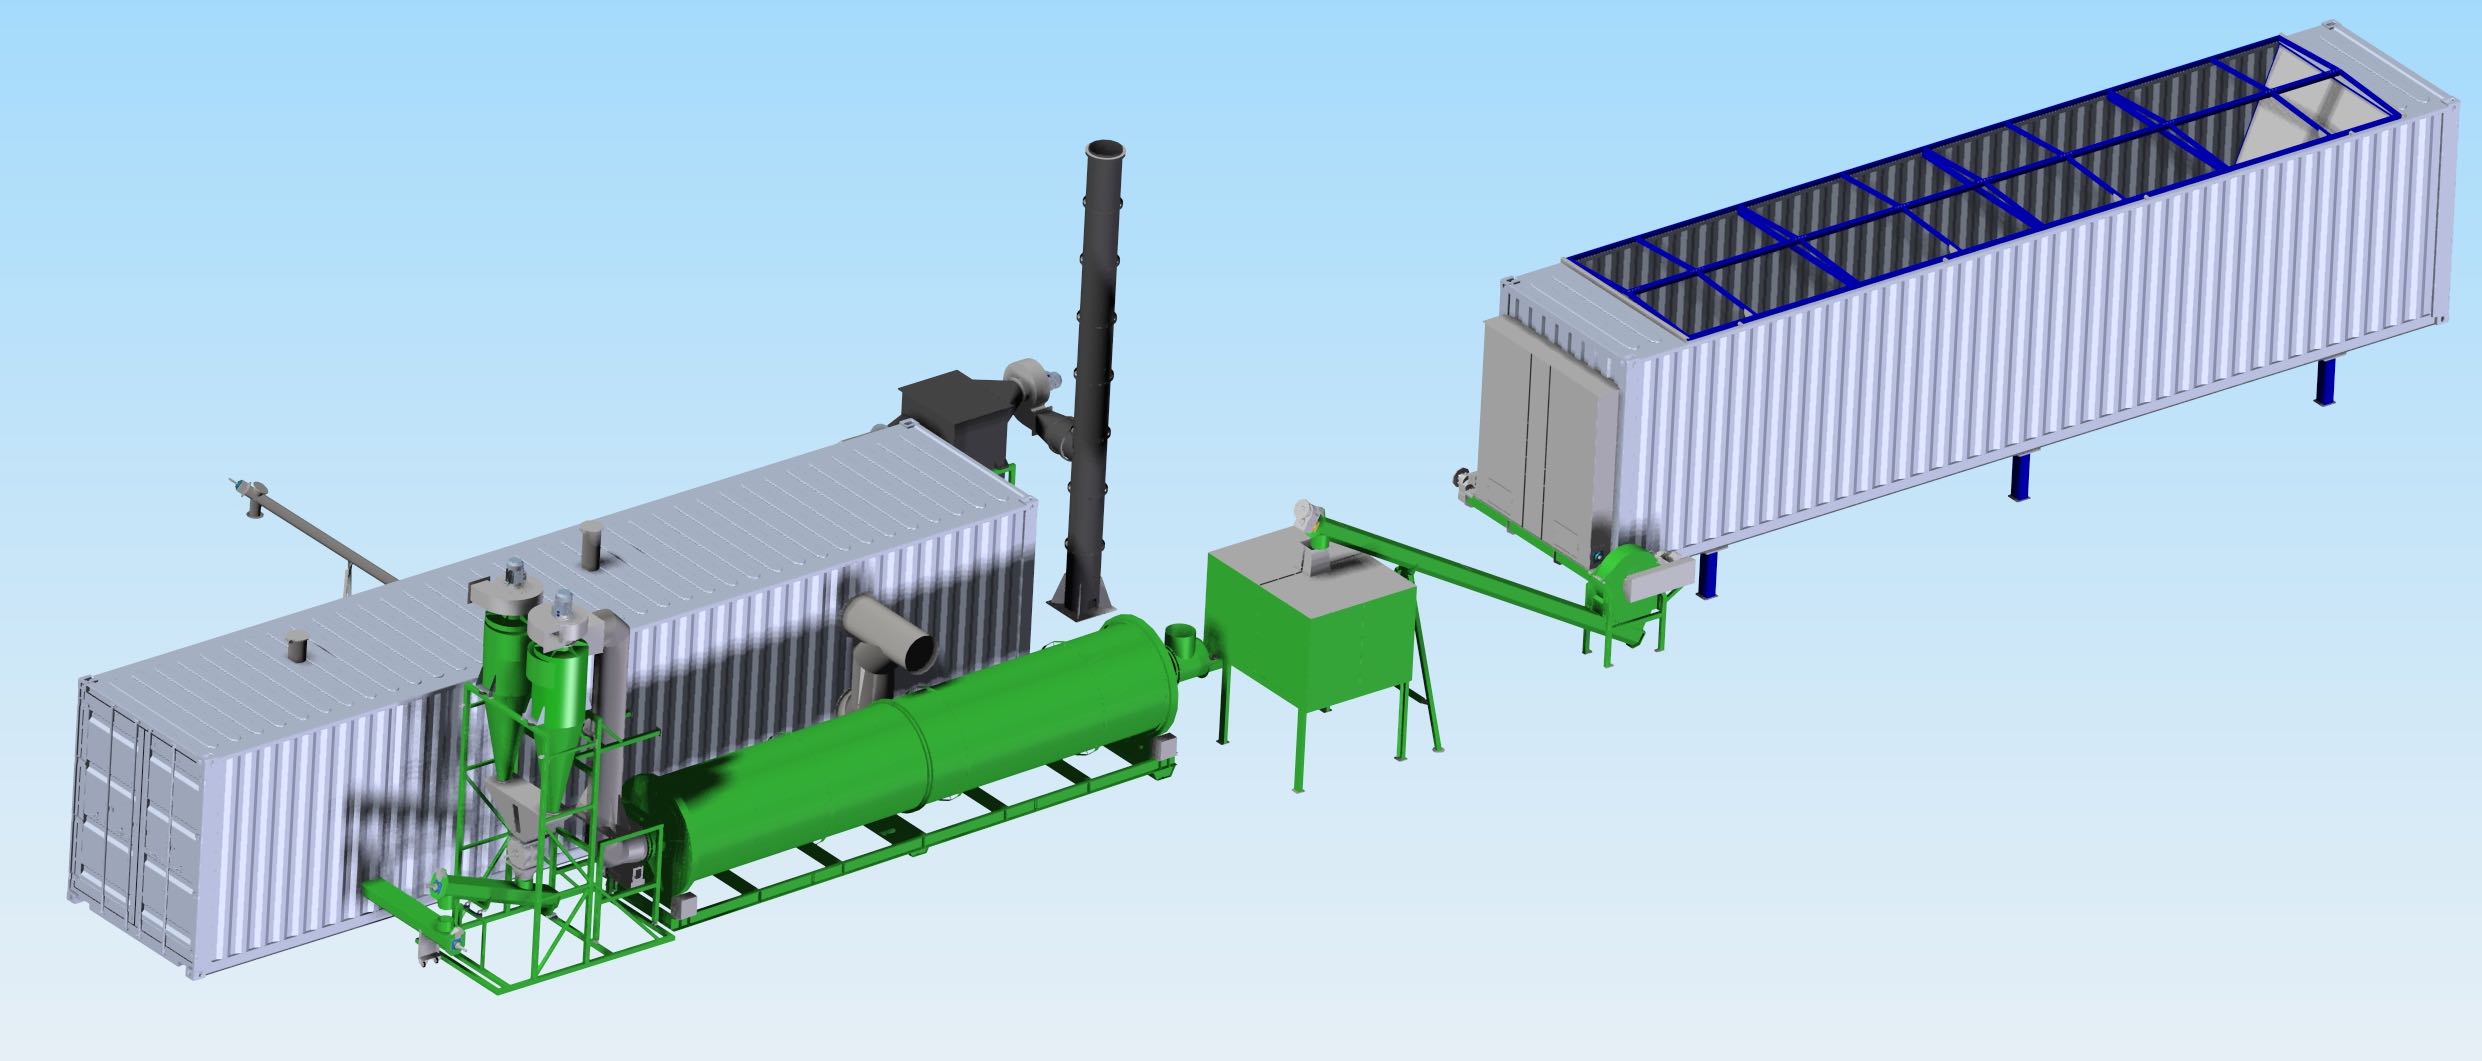
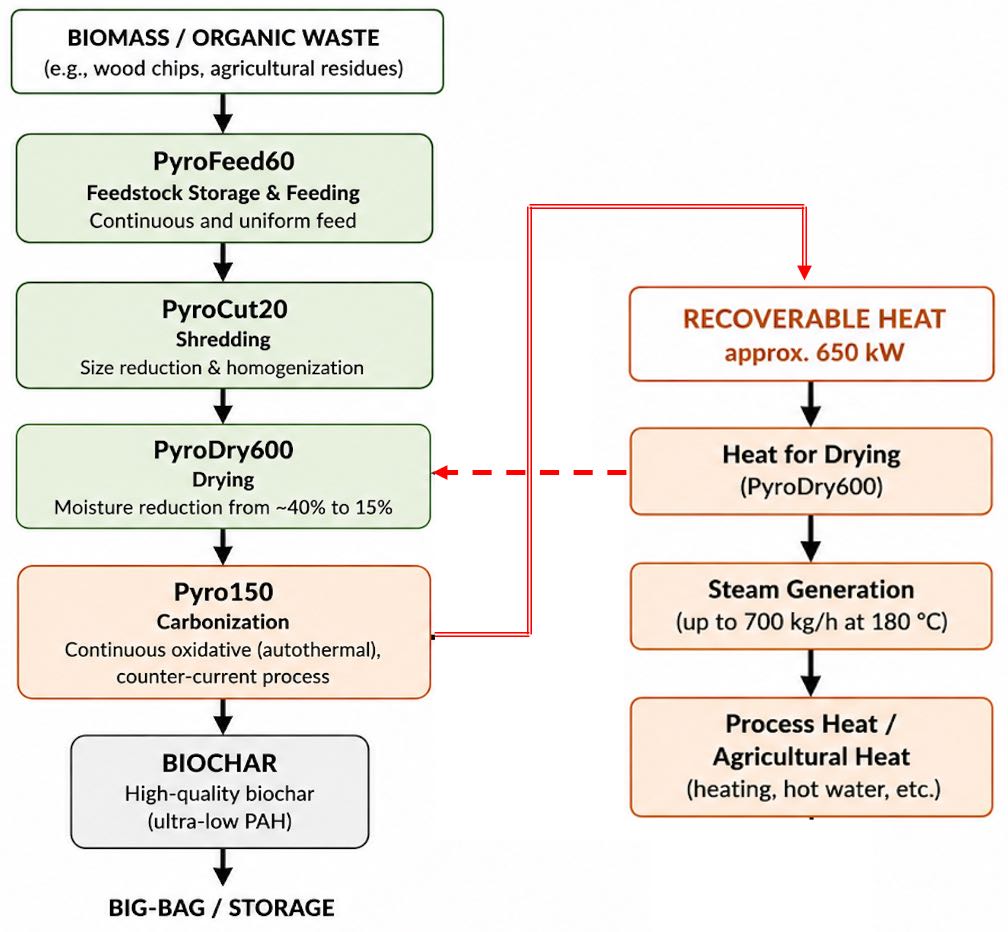
The system integrates biomass handling, preparation, drying and continuous carbonization in a coordinated industrial solution. Its modular structure supports both project flexibility and practical on-site implementation.
From incoming biomass to finished biochar, each stage prepares the material for reliable downstream operation.
Containerized biomass storage and controlled feeding.
Shredding and feedstock homogenization.
Pre-drying to the required carbonization moisture content.
Continuous carbonization, biochar discharge and energy recovery.
Selected indicative parameters from the PyroChar150 technical concept.
● Indicative design specificationsPerformance depends on feedstock, moisture, configuration and operating conditions. Final project specifications are confirmed individually.
| Biochar production capacity | 135–165 kg/h |
| Carbonizer biomass feed rate | Up to 600 kg/h |
| Feedstock moisture at carbonizer | ≤ 18% |
| Carbonization temperature | 400–700°C |
| Design recoverable heat | Approx. 650 kW |
| Feedstock storage | 18 m³ |
| Drying capacity | Approx. 700 kg/h |
| Carbonizer dimensions | 12 × 2.5 × 2.85 m |
| Carbonizer electric demand | 6 kW* |
| Flue-gas filtration | Combined electrostatic vortex-tube filter |
*Carbonizer only; excludes auxiliary units and site loads. Figures are indicative and not a contractual guarantee.
Illustrative reference values from the supplied technical material show how the system can convert dry biomass into biochar, recover useful waste heat and support several agricultural heat applications.
An illustrative process example shows 1 ton of dry biomass input (for example sunflower husk) being converted into approximately 230 kg biochar and 770 kg gases, vapors and other products in an autothermal, continuous pyrolysis process.
Sunflower husk: 23%
Wood chips: 25%
Rice husk: 30%
PyroChar 150: ≈ 650 kW
Biomass drying, manure drying, compost drying and other agricultural applications.
Reference examples include sunflower husk, wood chips and rice husk, highlighting flexible feedstock use.
These values are illustrative reference data taken from the supplied presentation material. Actual performance depends on feedstock type, moisture, system configuration and operating conditions.
PyroChar International Kft. supports the marketing, customer engagement and commercial coordination of industrial pyrolysis and biochar production systems.
We work with prospective industrial partners to understand feedstock streams, desired production capacity, mobility requirements, energy integration opportunities and project expectations. Equipment supply and commercial terms are agreed on a project-specific basis with the relevant parties.
Start a conversation ↗Tell us about your available feedstock, preferred output and project requirements. We will gladly support the next step in the technical and commercial discussion.
Send an email ↗